
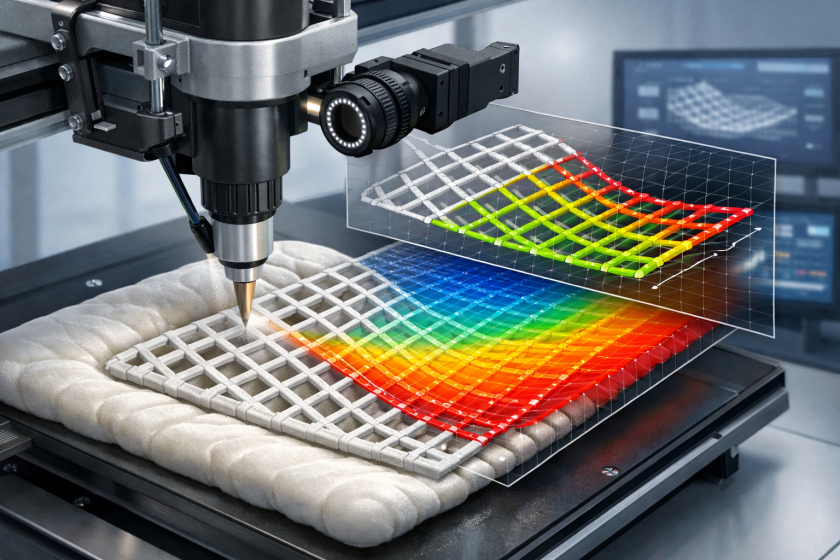
The notable IT shift here is not simply “AI for defect detection,” but the move from pass/fail inspection to in-process geometric metrology. That changes the architecture of an additive-manufacturing quality stack: image capture, segmentation inference, strand-tracing, and spatial mapping now become part of the production control loop rather than a separate post-process analytics task.
For practitioners, the hard problem is less model accuracy in isolation than end-to-end calibration. A few-micrometer measurement claim is only operationally meaningful if camera position, lens distortion, lighting, nozzle motion, and build-platform alignment are controlled as a single measurement system. In production, that implies versioned calibration routines, traceable reference artifacts, and drift monitoring alongside model retraining.
Scalability is the other key implication. Thousands of images per layer can quickly turn inspection into a throughput bottleneck unless inference, storage, and data reduction are designed upfront. Teams considering similar approaches should decide early which outputs must be retained long term: raw images, segmentation masks, derived geometry, or only exception events. That choice affects GPU placement at the edge, network bandwidth, historian design, and whether the system can support closed-loop correction during a print instead of after-the-fact diagnosis.
The broader opportunity is integration. If these diameter maps feed manufacturing execution, maintenance, and process-control systems, recurring patterns such as nozzle wear, stage misalignment, or material inconsistency can be correlated across jobs rather than treated as isolated defects. That is where machine vision becomes operational intelligence, not just automated inspection.
Researchers at Lawrence Livermore National Laboratory (LLNL) have developed a camera-based inspection system that uses AI and machine learning (ML) to check 3D printed parts while they are still being made. Existing ML approaches for monitoring additive manufacturing (AM) processes have focused mainly on detecting and classifying defects, rather than measuring a part’s actual geometry as it is built.
The work, published in npj Advanced Manufacturing, focuses on direct ink writing (DIW).
How the System Measures Parts
DIW deposits soft or paste-like materials through a nozzle in thin strands and can produce flexible cushions whose performance depends on the size and arrangement of those strands, some only a fraction of a millimeter thick. Small variations in filament diameter, center-to-center pitch, or the angle between strands can produce substantial changes in mechanical performance. Current inspection typically relies on X-ray computed tomography (CT) performed after the print is complete, or on surface-only optical methods that do not capture internal strand geometry.
In the LLNL setup, a camera mounted on the printer captures images as each layer is deposited. Software identifies the newest strands and calculates measurements such as filament diameter. ML-based image segmentation and computer vision tools convert the thousands of images collected during a build into detailed measurements and spatial maps of the deposited material.
The team trained the segmentation model on a curated dataset of nearly 13,800 human-annotated images covering several lattice geometries. A computer vision algorithm then used the model’s output to trace strands and measure their diameter. Across 55 test parts, the automated measurements were typically within a few micrometers of those made by people.
Mapping a Full Cushion
To test the system at scale, the researchers applied it to a cushion with a designed footprint of about 25 by 25 centimeters. They gathered around 2,420 images from a single layer and combined the measurements into a spatial map of the part’s interior.
The resulting map exposed a large-scale pattern in filament diameter spanning the print, one that an average measurement across the whole part could have concealed entirely. The pattern pointed to a slight tilt of the build platform relative to the nozzle.
The researchers noted that X-ray CT limits the size of an object that can be examined at high resolution, while a camera mounted on the printer can inspect parts larger than practical CT coverage allows.
Titled “Scalable on-machine inspection of direct ink write additive manufacturing,” the study was conducted by Brian T. Weston, Michael E. Zelinski, Hamed Ziad Ammar, Aldair E. Gongora, Brian Au, Robert Cerda, Joshua R. DeOtte, William Smith, and Brian Giera.
As-printed top-down images of SC and FCT lattices. Image via LLNL.
Bringing Measurement Into the Build Itself
DIW quality control has depended on post-print X-ray CT, which volume-resolution limits confine to small parts, or on surface-only optical methods that cannot see internal strand geometry, leaving no scalable way to measure filament-scale dimensional accuracy across a full part while it is still printing.
Ai Build‘s AiMaker platform, also a large-scale, extrusion-based system, moves quality checks into the build itself: a camera and GPU module compare images of an in-process part against previously printed objects and flag deviations in real time, instead of waiting for the finished piece. It shares the goal of catching problems before a large-scale extrusion print completes, but it detects visual deviation from a reference print, and it does not produce the continuous, part-level diameter maps the LLNL pipeline generates.
Both approaches move large-scale extrusion inspection into the print itself; the LLNL pipeline pushes that further into precise, filament-scale geometric metrology that a visual-comparison system does not attempt.
Register now for AMA: Software 2026. Join 3D Printing Industry on 22 October for expert presentations, panel discussions and live audience Q&A exploring the software shaping additive manufacturing. Register here.
To stay up to date with the latest 3D printing news, don’t forget to subscribe to the 3D Printing Industry newsletter or follow us on LinkedIn.
Explore the full Future of 3D Printing and Executive Survey series from 3D Printing Industry, featuring perspectives from CEOs, engineers, and industry leaders on the industrialization of additive manufacturing, 3D printing industry trends 2026, qualification, supply chains, and additive manufacturing industry analysis.
Featured image shows on-machine inspection pipeline. Image via LLNL.
Enjoyed this article? Sign up for our newsletter to receive regular insights and stay connected.